In the air separation industry, stable equipment operation is paramount. One leading air separation company, located in a coastal region, specializes in the separation and extraction of oxygen, nitrogen, argon, and other gases. Its production process involves liquefying air before separating components based on differences in boiling points, with heavy-duty centrifugal compressors playing a pivotal role throughout.
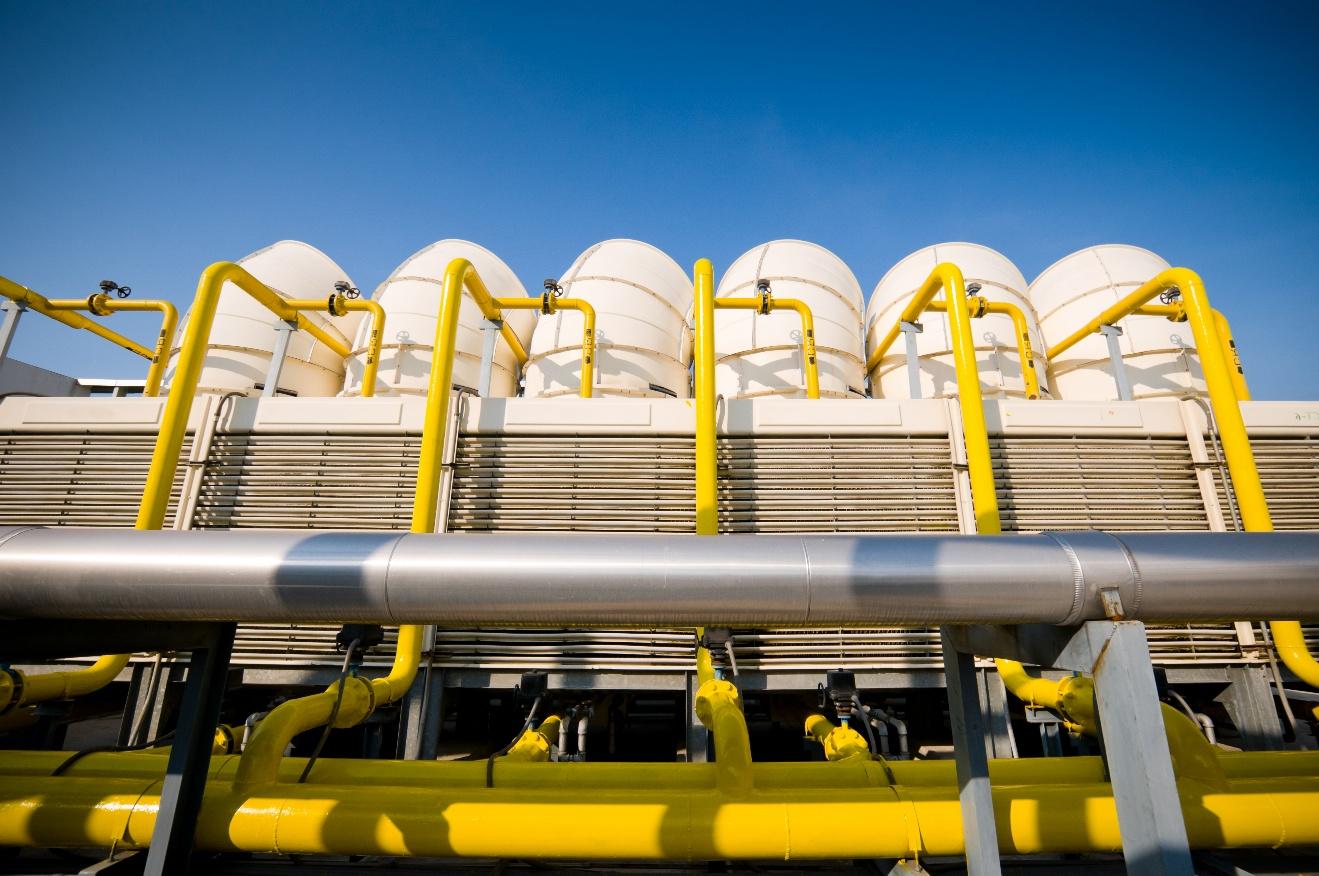
However, the company faced a persistent challenge. The heat exchangers — critical components spanning the entire air separation process and directly affecting system efficiency, energy consumption, and stability — suffered from severe fin powdering and flaking. The fins, continuously exposed to high-temperature, high-humidity, salt-laden gas environments, deteriorated rapidly. This not only drastically shortened the service life of the heat exchangers but also posed serious safety risks to the compressors. Finding a fin solution capable of withstanding such harsh conditions became an urgent priority for the company.
Upon learning of the client's difficulties, API Heat Transfer swiftly mobilized its R&D capabilities and developed a highly targeted solution. API innovatively applied fins coated with its proprietary Heresite coating, which delivers exceptional corrosion resistance in high-temperature, high-humidity environments — effectively armor-plating the fins with a robust protective shield.
In actual operation, heat exchangers equipped with Heresite-coated fins demonstrated service life more than three times longer than those using uncoated fins. The coating had zero adverse impact on heat transfer performance, ensuring high production efficiency while extending equipment life. Furthermore, the solution offered an excellent cost-to-benefit ratio well within the client's budget.
The implementation of API's Heresite-coated fin technology successfully resolved the severe corrosion issues plaguing the air separation company's heat exchanger fins in its coastal environment, significantly extending the overall service life of the air separation plant, enhancing operational stability, and reducing maintenance costs. The client expressed strong satisfaction with API's innovative solution — not only for resolving the immediate problem but also as a foundation for deeper collaboration. The company has since continuously expanded its partnership with API Heat Transfer across broader business areas.
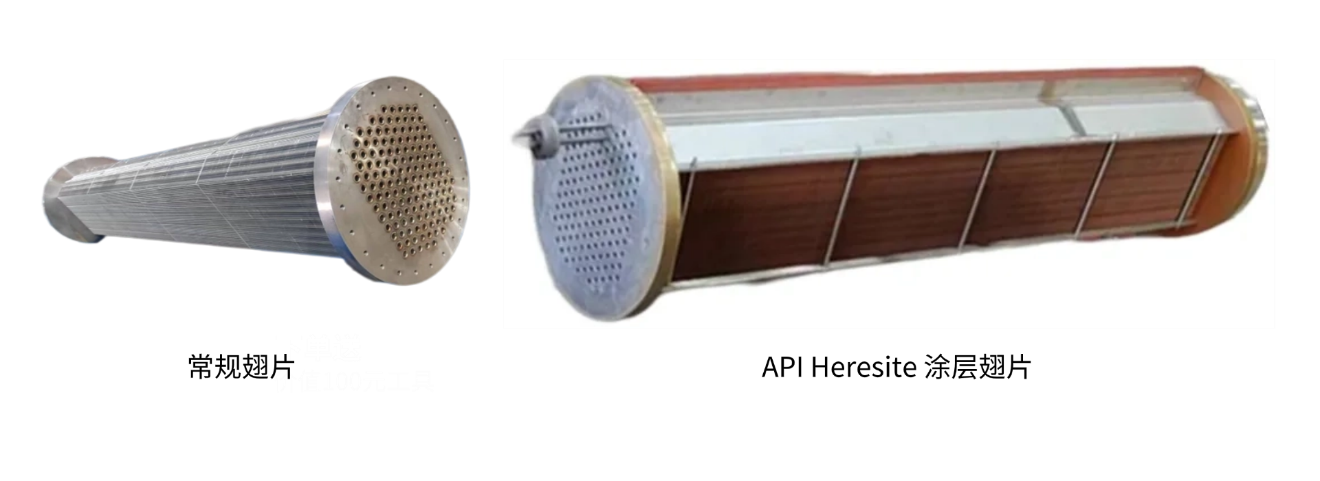
Key Advantages of API's Heresite-Coated Fin Technology:
API Heat Transfer's Heresite coating technology proves to the industry that fighting corrosion need not come at the expense of performance, and extending equipment life need not mean sharply rising costs. When technological innovation meets precision service, even the most demanding coastal environments can see exponential gains in equipment longevity. Going forward, API Heat Transfer will continue to drive innovation, delivering premium solutions to support the ongoing advancement of the air separation industry.
For more details, please visit API Heat
Transfer website or contact us

Suzhou Factory:
No. 156 & No. 126, Qingqiu Street, 3rd District, Suzhou Industrial Park, Suzhou, Jiangsu, China
Tel.: +86.512.88168000 - 5424


Suzhou Factory:
No. 156 & No. 126, Qingqiu Street, 3rd District, Suzhou Industrial Park, Suzhou, Jiangsu, China
Tel.: +86.512.88168000 - 5424
Shanghai Office:
No. 1699, Gubei Road, Minhang District, Shanghai, China
Tel.: +86.21.5426.2525

 Suzhou:+86.512.8816.8000
 API.China@apiheattransfer.com